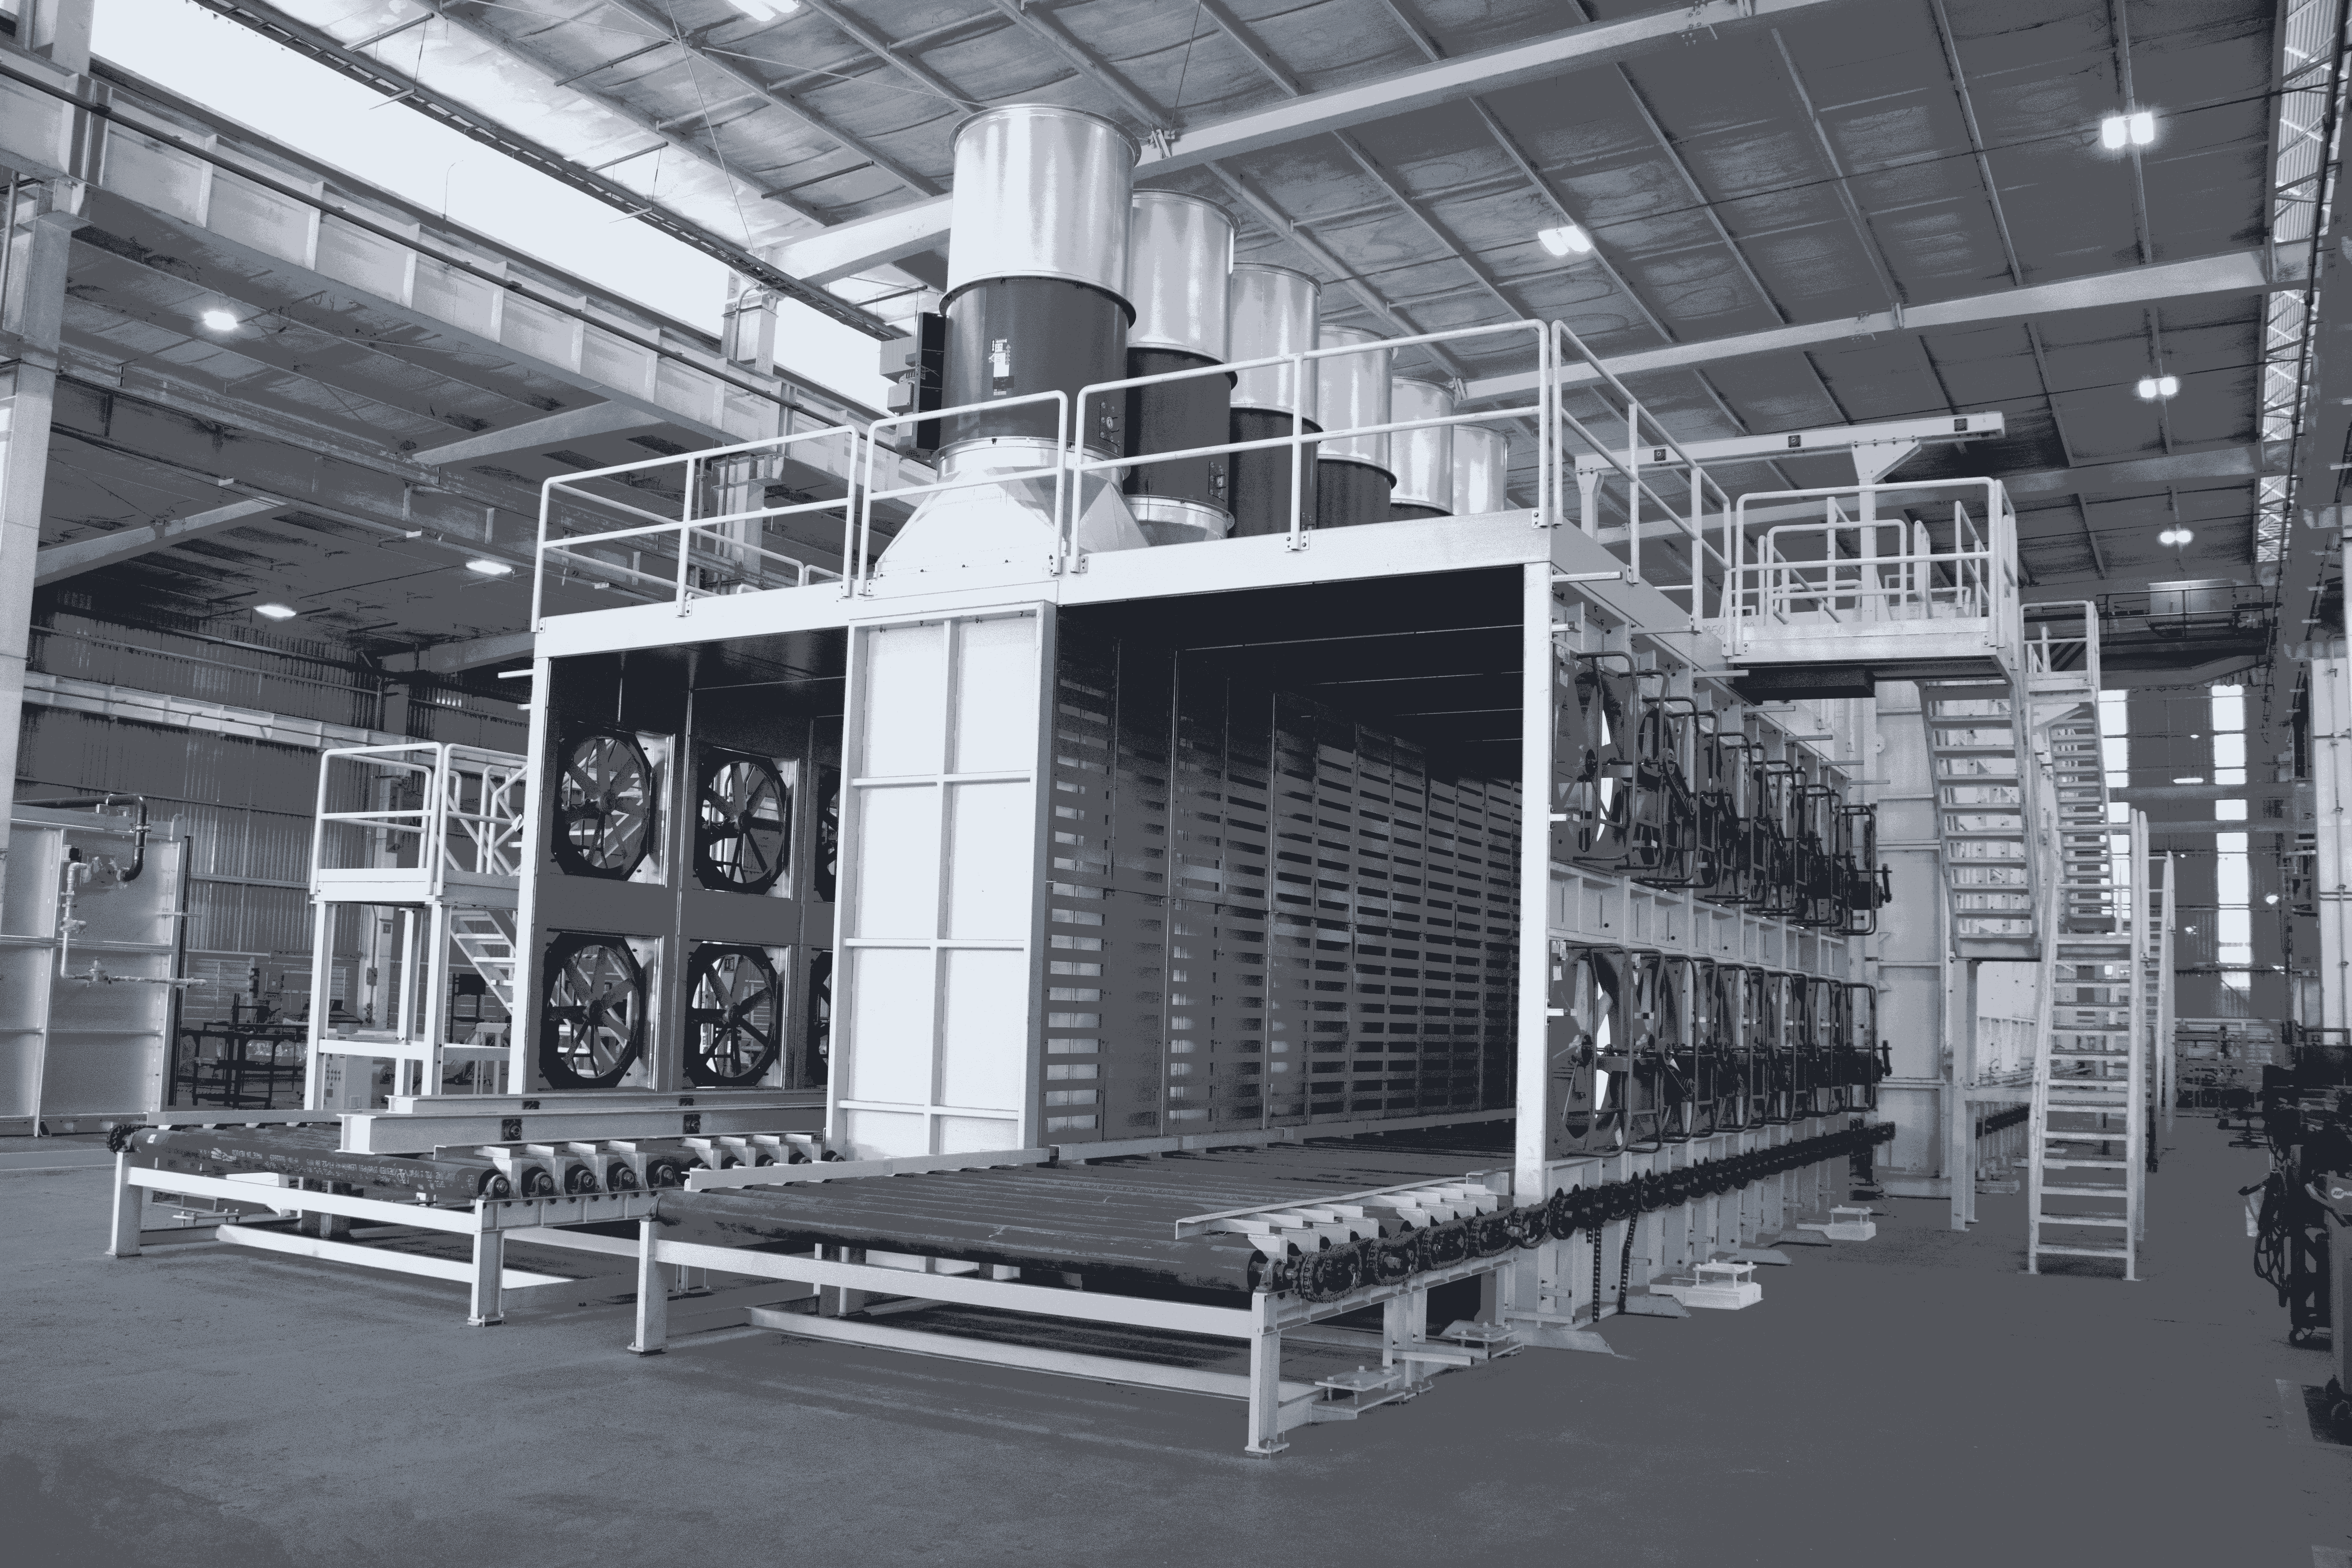
NUTEC Bickley is engineering and delivering a custom double-conveyor roller hearth aging oven for one of the most iconic and recognized automotive manufacturers in the world. This is the first project of this kind between NUTEC Bickley and this customer, and it represents exactly the type of engagement NUTEC Bickley was built for: a complex, highly customized thermal system, engineered from the ground up to meet the specific production requirements of a world-class industrial operation.
Aging Aluminum Automotive Parts: A Process That Doesn’t Forgive Deviation
Aluminum casting parts for automotive applications — suspension components, engine housings, structural brackets — undergo an artificial aging heat treatment after solution annealing to develop their final mechanical properties. It’s a precise, time-temperature process: the aluminum alloy is held at a specific temperature for a specific duration, and the precipitation hardening that occurs during that window determines the part’s final strength, hardness, and dimensional stability.
Get the temperature wrong by more than a few degrees and the metallurgy changes. Hold for too long or too short and the mechanical properties shift outside specification. For safety-critical automotive components, that’s not an acceptable outcome — which is why the temperature uniformity requirement on this oven is ±5°C throughout the working chamber during soak, verified to CQI-9 standard.
That standard — CQI-9, the automotive industry’s heat treatment system assessment — is the benchmark the industry holds its thermal equipment to. Designing an oven that meets it, at the throughput this customer requires, across a double-conveyor layout running continuously around the clock, is the kind of engineering challenge NUTEC Bickley takes on by design.
The Project: A First Collaboration Built to Last
The oven is a double-conveyor roller hearth system — two independent conveyor lanes running in parallel through a single chamber — with a total line length of 82.33 feet. The system processes aluminum automotive casting parts, with two baskets entering the oven every 7.58 minutes. Each basket carries up aluminum parts plus a steel basket, for a total load weight of nearly 2,000 lb per basket position. At any given moment, twenty baskets are inside the oven, ten per conveyor, cycling continuously through the heat treatment Process.
How the Oven Is Built?
Structure, Insulation, and Doors
The oven shell is fabricated from carbon steel plate on a structural steel frame, designed for the thermal and mechanical stresses of continuous industrial operation. The insulation system uses 6-inch mineral fiber modules at 8 lb/ft³ density, retained between inner and outer steel sheets with all panel joints packed to minimize heat transfer. The result is a well-insulated, thermally stable chamber that holds temperature uniformly across both conveyor lanes and the full working height of the load.
The four vertical lift doors — two at the oven entrance, two at the exit — are built to the same insulation specification as the walls and operate on pneumatic lifting and sealing systems. Each door clamps to the furnace frame pneumatically when closed, with a ceramic fiber perimeter seal for positive closure. A manual lock in the raised position allows safe work under the door when needed.
Heating System: Electric, Precise, and Built for Continuous Operation
The oven is electrically heated with low-density Incoloy-sheathed tubular heating elements — installed behind air circulation baffles and not exposed to the load — across 22 banks, 11 per side, positioned at both walls for balanced heat input. With a total installed thermal capacity of 1,350 kW, the heating system is sized for the thermal mass of the load and the throughput rate, with SCR power control for precise, stable zone-by-zone temperature regulation.
Eleven independent temperature control zones span the full length of the oven, each with its own control thermocouple and dedicated high-limit protection. That zone density is what makes ±5°C uniformity achievable at this load weight and conveyor speed — it gives the control system the resolution to compensate for the thermal variation that a load of this mass introduces as it moves through the chamber.
Air Recirculation: The Engineering Behind Uniformity
Temperature uniformity at ±5°C doesn’t happen by accident — it’s the result of a carefully engineered air recirculation system. Eleven centrifugal plug fans — belt-driven, high-efficiency TEFC motors with variable speed drives — recirculate hot air horizontally through the load in a forced cross-flow pattern designed to deliver consistent heat exposure to every part on every basket, regardless of position in the chamber.
The plug fan design integrates directly into the plenum system, keeping the overall oven footprint compact while maximizing the convective heat transfer efficiency that aluminum aging requires. Steel baffles direct the airflow precisely through the load zone, and the variable speed drives allow the recirculation rate to be tuned to the specific basket configuration and product geometry.
Conveyor System
Two independent roller conveyors run through the oven simultaneously, each with its own drive, VFD, bearings, sprockets, and chain drive. The rollers are sized for the basket weight and designed for long-term continuous operation at operating temperature. At the entrance and exit, four external roller conveyors — each holding three basket positions — buffer the flow between the oven and the plant’s loading and unloading operations. Safety laser scanners at the loading and unloading positions protect personnel from conveyor movement during those operations.
Integrated Cooling Tunnel
Immediately following the aging oven, an integrated cooling tunnel brings the aluminum parts from 225°C back to a safe handling temperature before they exit the system. The tunnel accommodates twelve basket positions — six per conveyor lane — providing 57 minutes of cooling time at production throughput rate.
The parts that exit have been aged precisely and cooled predictably — ready for the next step in the manufacturing process.
Controls and Automation
A central PLC manages all eleven heating zones, conveyor drives, fan speeds, door operations, and safety interlocks from a single 10-inch HMI touchscreen. Zone temperatures, equipment status, and process alarms are visible at a glance. A paperless recorder logs all eleven zone temperatures continuously for process traceability — a requirement that CQI-9 makes non-negotiable. Independent high-limit controllers on every zone provide a dedicated safety layer, cutting heating power automatically if any zone approaches an unsafe condition.
A Word from NUTEC Bickley Leadership
“This project is the kind that defines a company. When one of the most recognized automotive brands in the world selects NUTEC Bickley to engineer a system like this — a highly customized, continuous heat treatment line built to their specific standards, for a process where the metallurgical outcome determines part performance — it means something. It means that our engineering capability, our execution track record, and our understanding of what precision industrial equipment really requires have been evaluated and found equal to the task. We don’t take that lightly. We were built for exactly this kind of project, and we intend to deliver something this customer will be running on their production floor for a very long time.”
— Arturo Arechavaleta, VP Metal, NUTEC Bickley
When the Project Is the Statement
There are projects that fit neatly into a portfolio, and there are projects that define what a company is capable of. This is the second kind. A double-conveyor roller hearth aging system, built to automotive-grade standards, engineered for a manufacturer whose quality requirements are among the most rigorous in the global industrial landscape — this is not a project that any thermal equipment supplier can take on.
NUTEC Bickley can. And does. The engineering team, the manufacturing capability, the depth of experience in continuous heat treatment systems for the metal industry — it all comes together in a project like this one. This is what we were built for. And we are proud to be building it for one of the most iconic names in American manufacturing.
Looking for a thermal equipment partner for your next demanding project?
Let’s talk. → sales@nutec.com